



Specifying slit coils: what to put on the purchase order
Most problems with slit coils come from requirements that were assumed but never written down. This checklist covers the dimensions and coil details to agree before slitting starts.
A slit coil looks simple, but its usefulness on your line depends on more than grade and width. Core-cutting lines, stamping presses and transformer winding equipment each have limits on coil size, weight and edge condition. Writing them on the order lets us plan the slitting pattern and packing before the master coil is cut.
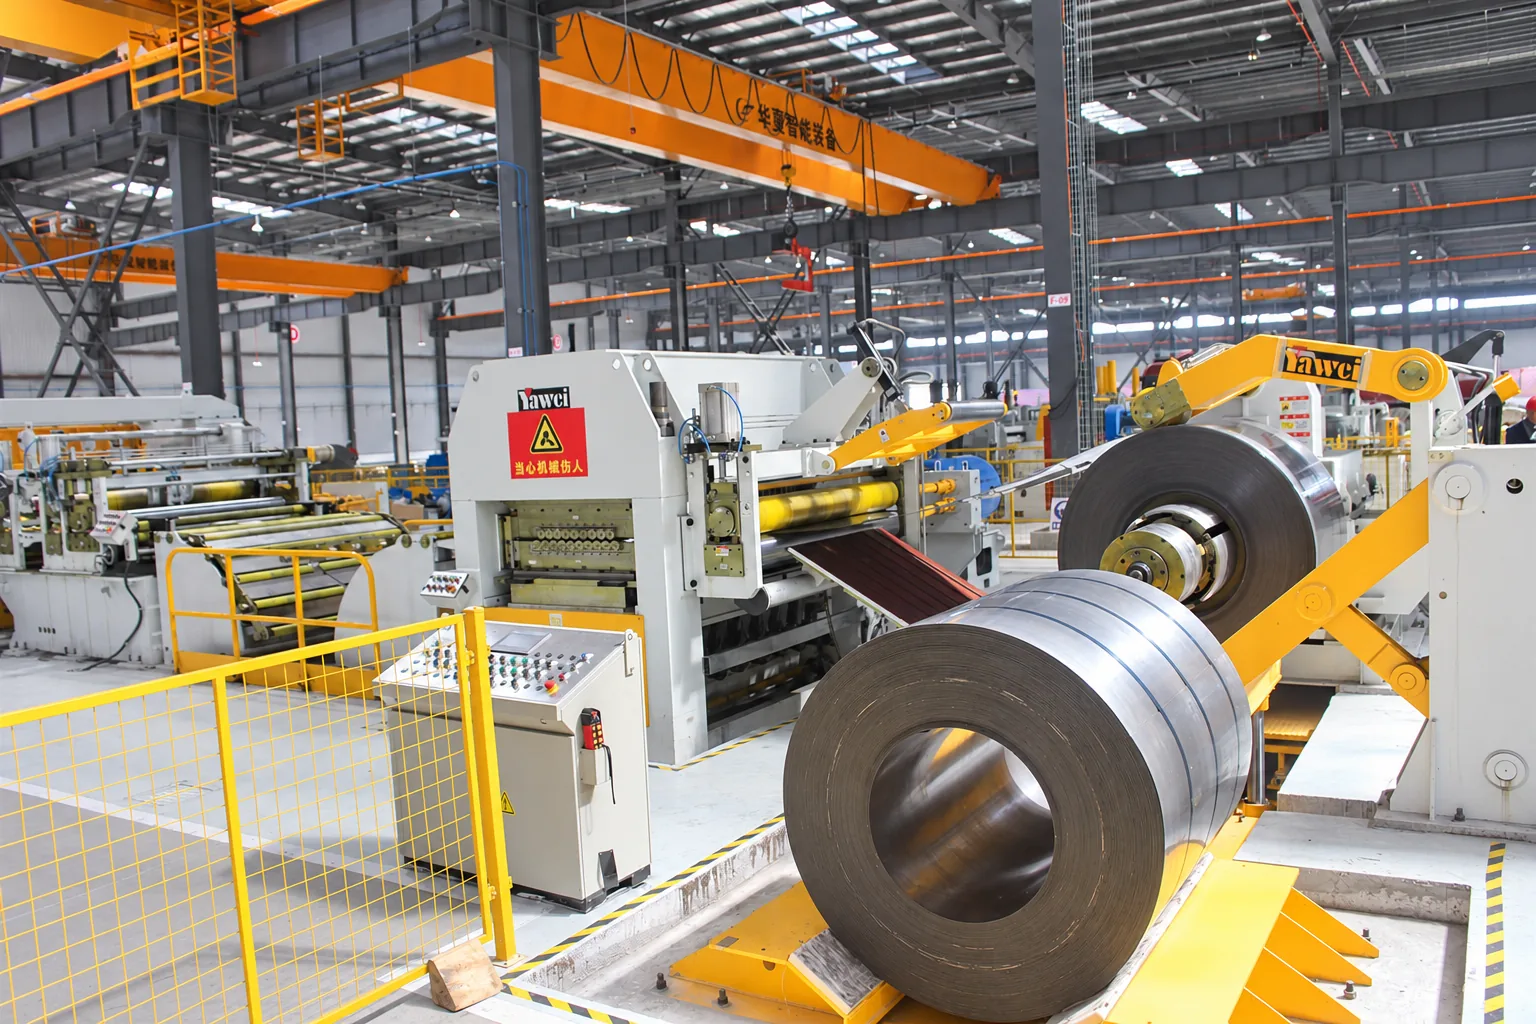
How a slitting plan is made
Baosteel master coils are typically around 1,000 to 1,250 mm wide. We combine the widths you need across that width so that the edge trim is as small as possible, and we keep the edge strips of the master coil out of critical widths where flatness matters most. If you order several widths, telling us which ones can share a master coil reduces scrap and therefore cost.
Dimensions
- Slit width and the tolerance you need. State it in millimetres, for example ±0.1 mm, rather than as a general class.
- Maximum burr height, measured to an agreed method.
- Camber (edge straightness) over a stated length, important for long transformer laminations.
- Thickness is set by the master coil; if you need a tighter thickness band than the standard, say so before we allocate material.
Burr and camber in practice
Burr is the raised edge left by the knives. On a transformer core, burrs on stacked sheets can bridge the insulation between laminations and raise the loss, so many core makers set a maximum of a few hundredths of a millimetre. Camber is usually stated over a 2 m length. A long lamination for a large power transformer needs a tighter camber than a short strip for a small motor core, so the limit should follow the part, not a general rule.
Coil details
- Inner diameter to suit your decoiler mandrel, commonly 508 mm.
- Maximum outer diameter and maximum coil weight your equipment can handle.
- Whether joins (welds) are acceptable inside a coil.
As a reference, Baosteel’s standard for grain-oriented strip for ultra-high-voltage transformers (Q/BQB 486) sets the coil bore at 500 to 520 mm with 508 mm recommended, and allows at most two marked joints per coil, at least 200 m apart. If your line cannot accept any joint, write “no joints” on the order.
Documents and labels
Tell us which identifiers you need on each label: your part number, purchase order number, grade, size and the source coil number. Each slit coil ships with the mill certificate of its master coil and our inspection report, so your incoming inspection can match label, certificate and report in one step.

