


Step-lap cutting for transformer cores: why the joint matters
In a stacked core, the corner joints are where the flux has to leave the rolling direction. Step-lap joints spread that transition over several layers and help keep no-load loss and noise down.
Grain-oriented steel has its lowest loss when the flux runs along the rolling direction. At the corners of a stacked core, the flux must pass from one lamination to the next across the joint. In a conventional mitred joint every layer is cut at the same position, so the air gaps line up and the flux crowds into the neighbouring sheets, which raises local loss, magnetising current and noise.
How step-lap works
In a step-lap joint the 45° cuts of successive laminations are shifted by a small offset, usually in groups of several steps. The gaps no longer line up, so the flux can bypass each gap through the overlapping sheets. Compared with a single-step mitred joint, this usually lowers the no-load loss and noise of the finished core; the exact effect depends on the core design, the number of steps and the overlap.
What we do at our plant
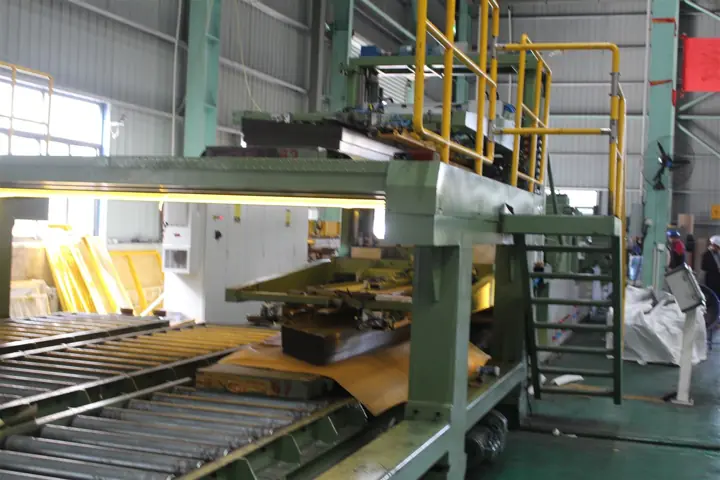
- Grain-oriented strip from 0.18 to 0.30 mm cut into 45° mitred and step-lap laminations to your core drawing
- Laminations grouped in stacking order, ready for the core shop
- Three-phase 3-limb and 5-limb cores stacked to drawing, delivered bare or with clamping frames
- Dimensions and stack height checked with CMM, vision measuring and height gauges
What to send for a quote
Send the core drawing with limb and yoke widths, stack height, number of steps and overlap, the grade (for example Baosteel B23P090 or B27R095), the quantity and the destination. We will confirm the cutting plan, material and price in a formal quotation.

