

12 coils of 50W800 slit strip to Mundra: a trial order followed by delivery in 40 days
One 20-foot container carried 12 coils of 50W800 non-oriented electrical steel, 0.50 mm × 360 mm, weighing 27.4 t, to Mundra, India. The case covers trial approval, slitting, inspection, packing, loading and documents.
Five key points
- Delivery depended on the slitting plan, packing, loading and documents, rather than unit price alone.
- A trial starting from one slit coil allowed the end user to approve the material first.
- A 1,250 mm parent coil yielded 3 × 360 mm plus a 170 mm strip; the three main strips represented 86.4% of the width.
- Five rows occupied 5 × 1.15 = 5.75 m of a 5.90 m container; coils 11 and 12 were stacked at the closed end.
- Check APTA eligibility and BIS requirements before shipment; the importer must confirm applicability.
Order at a glance
50W800 is a general-purpose non-oriented grade, 0.50 mm thick, with a P15/50 limit of 8.00 W/kg at 1.5 T and 50 Hz. This order was for EI laminations and small transformer cores. The difference between suppliers lay in execution, not a new metallurgical development.
| Item | Details |
|---|---|
| Buyer | Indian trader serving small transformer makers; no in-house processing |
| Destination | Mundra, India |
| Product | 50W800 non-oriented electrical steel slit strip |
| Dimensions | 0.50 mm × 360 mm; ID 508 mm; 2.26–2.35 t per coil |
| Quantity | 12 coils / 27.4 t / 1 × 20-foot GP |
| Application | EI laminations and small control transformers |
| Acceptance criteria | P15/50 ≤ 8.00 W/kg; burr ≤ 0.02 mm; width ±0.2 mm |
| Packing | Rust-preventive paper, sealed film, black straps and custom timber cradles (ISPM 15) |
| Terms | FOB; T/T 30% advance and 70% before dispatch |
| Delivery | Enquiry in early September 2026; collection in mid-October; 40 days |
| Outcome | Accepted in one delivery; no claim; next container requested |
The buyer was buying reliable delivery
The buyer was an Indian steel trader serving small transformer makers and stamping plants, without its own processing operation or inventory. It compared measured properties, schedule reliability, correct documents and responsiveness before price. A late delivery could stop production, a document error could incur demurrage, and an incorrect label could cause rejection. These risks outweighed a small saving in unit price.
Quality was established by the trial
The customer had previously bought a small trial batch for stamping. The end user checked burr height, lamination flatness and core loss. The repeat test gave 7.7 W/kg against an 8.00 W/kg limit, a margin of 0.3 W/kg; burrs and shape also passed. No additional customer or third-party pre-shipment inspection was requested for this order: the instruction was to follow the previous standard. The trial reduced the end user's uncertainty before the commercial order.
Slitting: putting the 170 mm remainder to use
The parent coil was 1,250 mm wide. Cutting 3 × 360 = 1,080 mm left 170 mm. Selling the remainder as scrap would increase the effective cost of the main strips. Another EI-lamination customer needed 170 mm strip that month, so the buyer selected the strip-sales option after comparing both cost scenarios. At 0.50 mm, the material was at the top of the stated 0.18–0.50 mm incoming range. The slitting line ran at 80% speed to control load and tension, adding half a day for the 12 coils.
Comparing total cost
The buyer compared several Chinese suppliers using price plus arrival risk, document rework and communication costs. HXES supplied four practical measures: a quotation with the 3 × 360 mm cutting plan, 86.4% width allocation and two options for the 170 mm remainder; a one-coil trial, reducing validation material from 5 t to about 2.3 t; timber cradles grooved to the coil diameter, addressing earlier failures of generic pallets; and loading at the factory before trucking the sealed container to port, avoiding an extra handling step.
Packing for the Mundra route
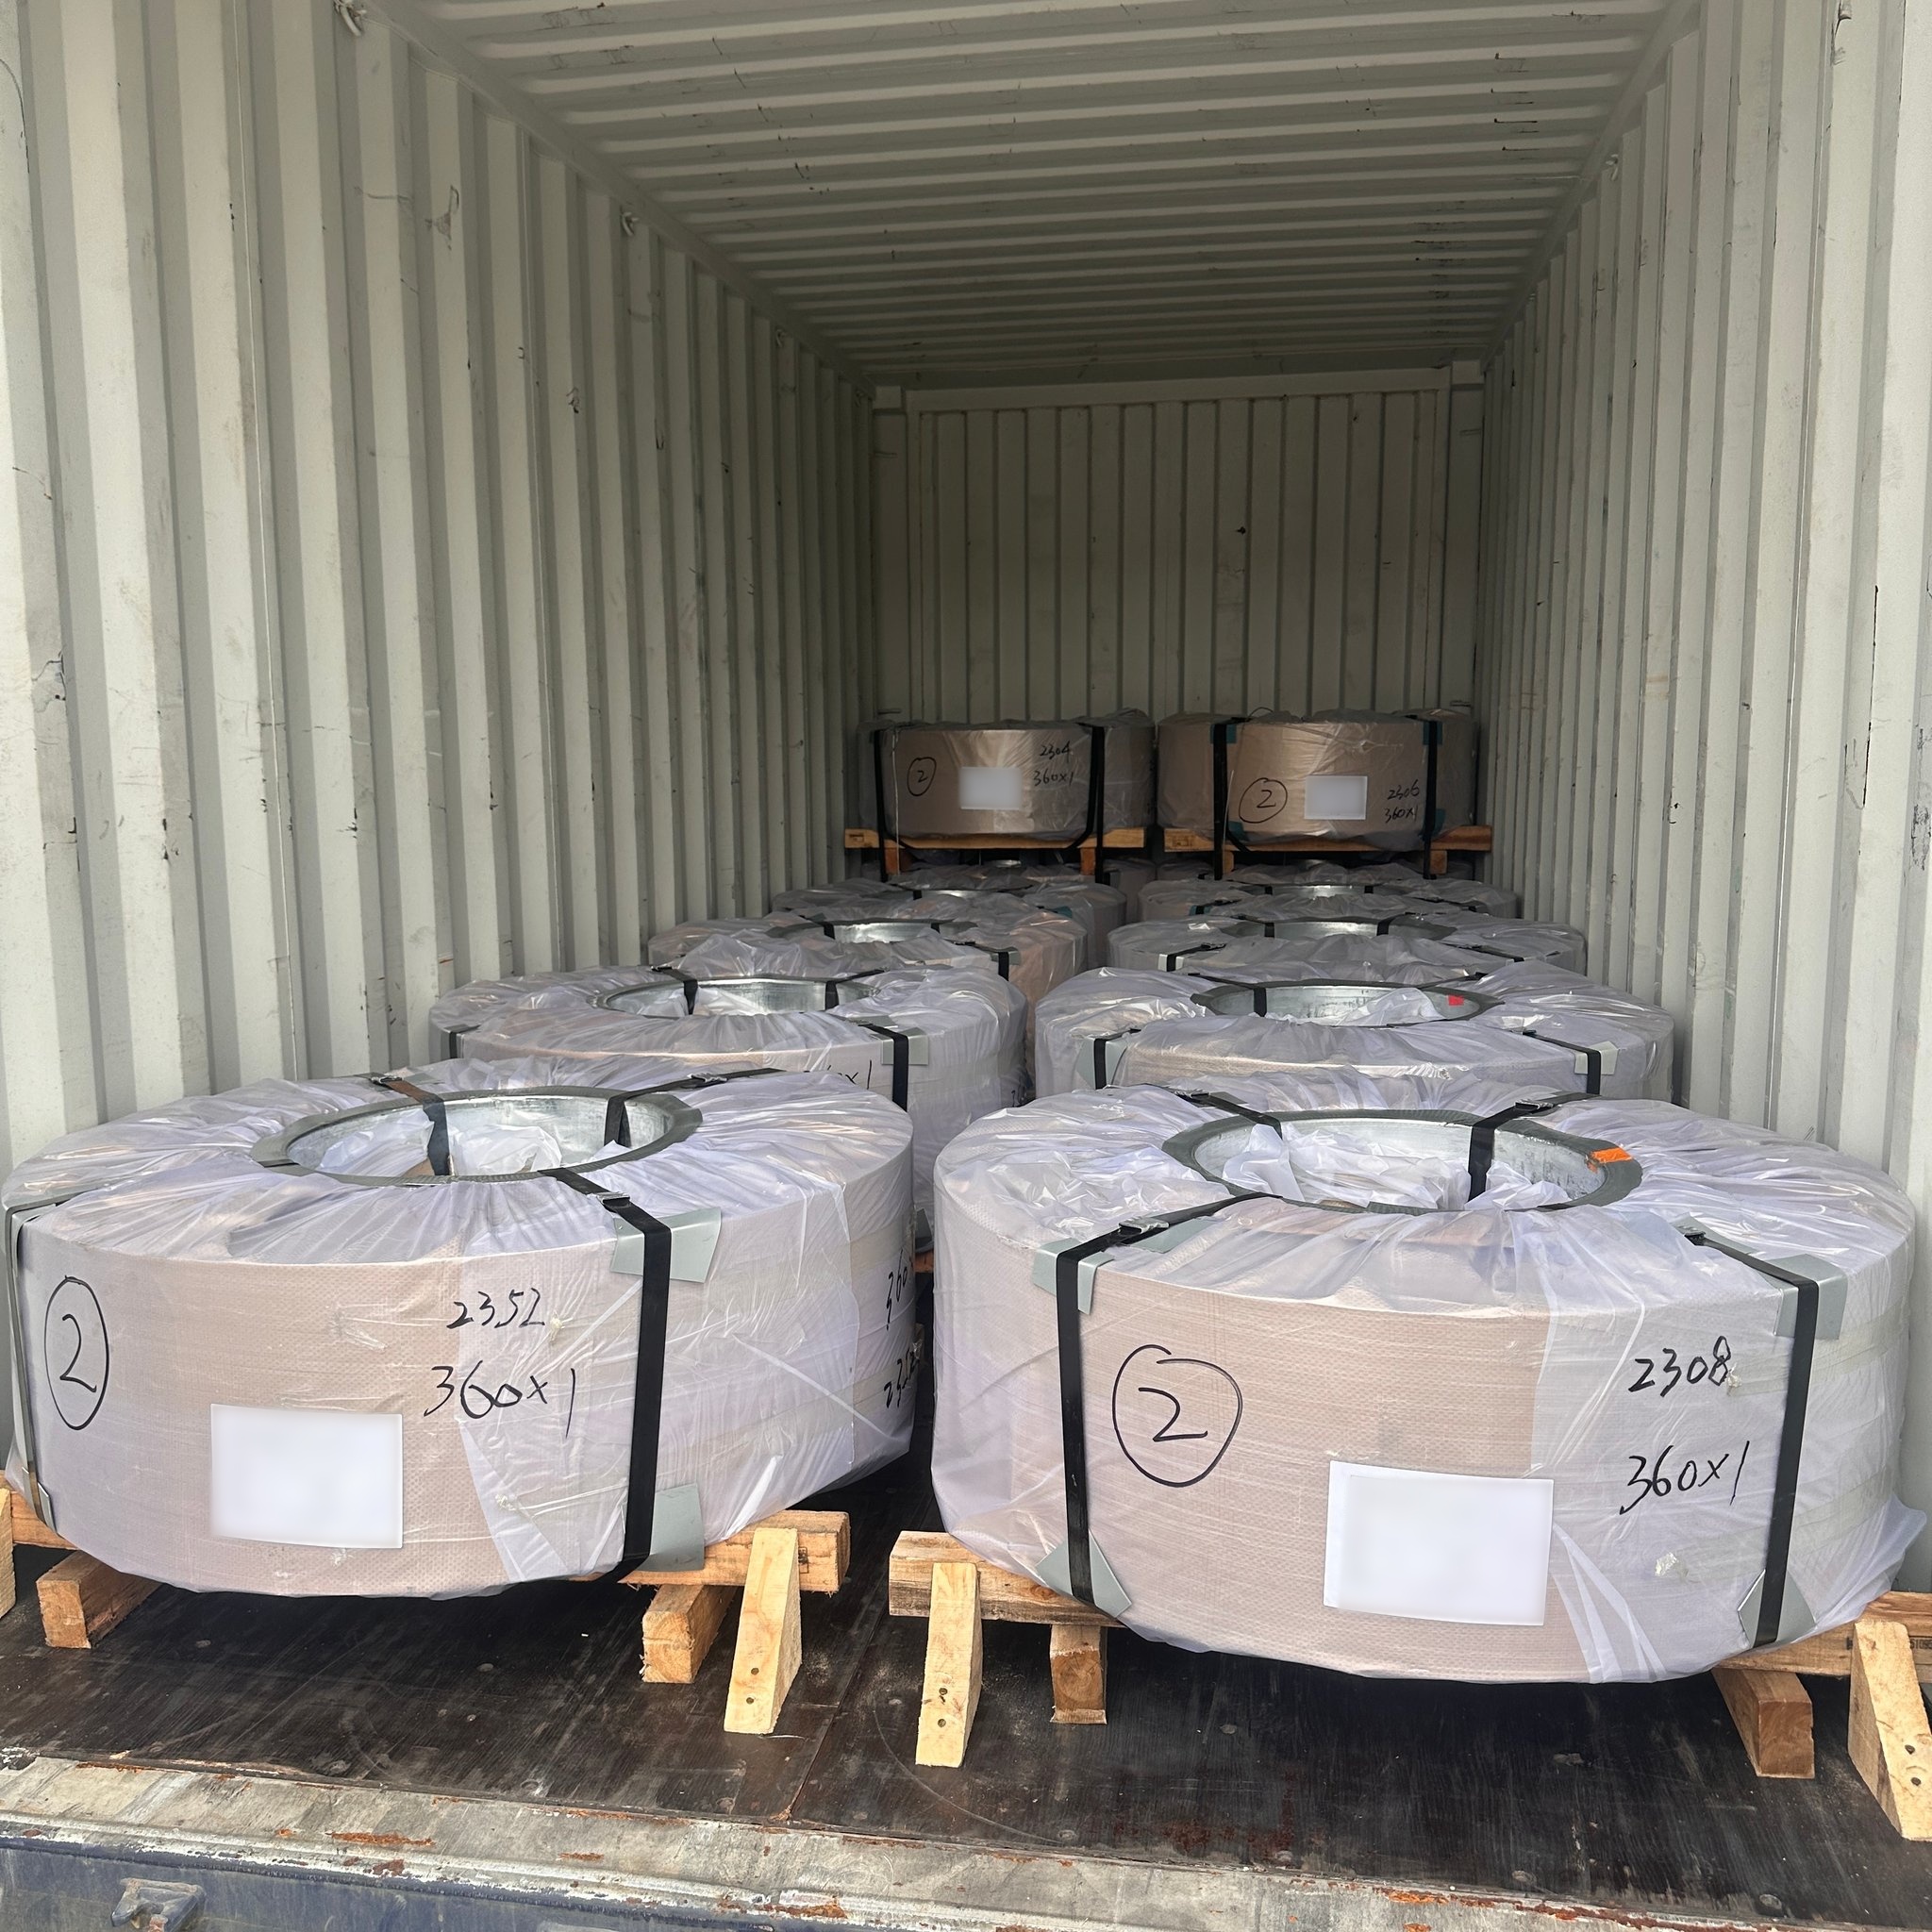
The stated sea passage from China to Mundra was 15–20 days. Temperature changes and condensation required coordinated protection: VCI rust-preventive paper against the steel; a fully enclosed plastic film with heat-sealed edges and two desiccant bags at each end of the coil bore; two longitudinal and two circumferential black straps on each coil, supported on the cradle; and purpose-made grooved timber cradles. Upper cradles bear on the lower supports when stacked. The timber was heat-treated to ISPM 15, IPPC-marked, and accompanied by a declaration. Clear marking photographs were included for inspection.
Loading: ten coils on the floor
The stated internal container dimensions were 5.90 m × 2.35 m, and coil outside diameter was 1.15 m. Five rows used 5.75 m, leaving 0.15 m; two columns used 2.30 m, leaving 0.05 m. Ten coils sat on the floor and two were stacked at the closed end. The reported remaining vertical clearance was 1.6 m. Cargo weight was 27.4 t. The actual container plate, total timber and packing weight, floor loading and carrier requirements must determine the loading plan. Loading proceeded from the closed end to the doors; stacked coils must be unloaded first.
Documents: FOB still requires coordination
Under the agreed FOB arrangement, the buyer nominated the forwarder and paid sea freight and insurance; HXES coordinated stuffing, inland transport and export customs. Six documents were checked: commercial invoice, packing list, bill of lading, certificate of origin, mill certificate and timber-packaging declaration. The consignee and bill-of-lading type were confirmed twice against written instructions. APTA preferential treatment depends on the HS code, origin rules and rules applicable at import. The importer or customs agent must check applicable QCO, BIS licensing or exemptions against product standards, HS code and use. The ISPM 15 declaration must match the marks. All six documents were confirmed three days before sailing.
Delivery timeline
Self-inspection found that coil 7 had a faint identification print. All 12 labels were reprinted, taking another 40 minutes. For a trader's end customer, correct identification is the first link in traceability.
| Stage | Period | Action |
|---|---|---|
| D0 | Early September | Enquiry with the end user’s grade and dimensions |
| D2 | — | Quotation, cutting plan and packing proposal supplied together |
| D5 | — | Supplier comparison and two technical clarifications |
| D8 | — | Order; 30% T/T received; parent coil and heat identified |
| D10 | — | Slitting: 3 × 360 + 170 mm |
| D10–D18 | — | Slitting, burr inspection, paper and film protection, timber cradles |
| D19 | — | Check width, burr, thickness, labels and mill certificate |
| D20 | — | 70% balance received |
| D21 | — | Load 12 coils at the factory, seal and photograph |
| D23 | — | Truck to port, clear export customs and sail |
| D40 | Mid-October | Customs clearance and customer collection in Mundra |
Results
The shipment was delivered without a claim or discount, and the customer requested a quotation for the next container. Its feedback was that the price was not the lowest, but having the plan, documents and packing arranged together avoided repeated questions.
| Metric | Result |
|---|---|
| Delivered quantity | 12 coils / 27.4 t, matching the packing list |
| Core loss | Sample checks: 7.6–7.9 W/kg, below 8.00 W/kg |
| Width and burr | Width within ±0.2 mm; burr ≤0.02 mm; all inspected |
| Packing | Paper and film intact; ISPM 15 records complete; no rust on opening |
| Sailing | Sailed on schedule; no reported demurrage in Mundra |
| Commercial outcome | No claim or discount; enquiry for the next container |
About HXES
Guangzhou Huaxin Industrial Co., Ltd. (HXES) is registered in Guangzhou, where sales, export documentation and customer service are handled. Processing is carried out at the Hunan site. Tonnage, coil count and milestones are based on this order's packing and production records; test values refer to the batch mill-certificate inspection records. Available quantities remain subject to inventory and production scheduling.
| Item | Details |
|---|---|
| Entity | Guangzhou Huaxin Industrial Co., Ltd. (HXES); Guangzhou sales, export documents and service |
| Processing site | Hunan; approximately 10,000 m²; slitting, cut-to-length/step-lap cutting, stamping and core stacking |
| Incoming material | 0.18–0.50 mm thick; maximum incoming width 1,250 mm |
| Tolerances | Slit width ±0.2 mm; burr ≤0.02 mm |
| Supply forms | Parent coils, slit coils, cut sheets and finished cores |
| Quality documents | Mill certificate with heat number and measured P17/50 or P15/50 and B8; dimension report; packing list; loading photos |
| Contact | Quotations/technical: kristy@huaxinelecsteel.com; orders/documents: michael@huaxinelecsteel.com |

